Moulding. Controlled conditioning. Final assembly.
This automotive sub-assembly combines two Nylon-66 mouldings, three plain-bore bracket inserts and a centre pin. Parshwa Plastics moulds and conditions the components, applies the lever sticker and completes the pin assembly in-house.
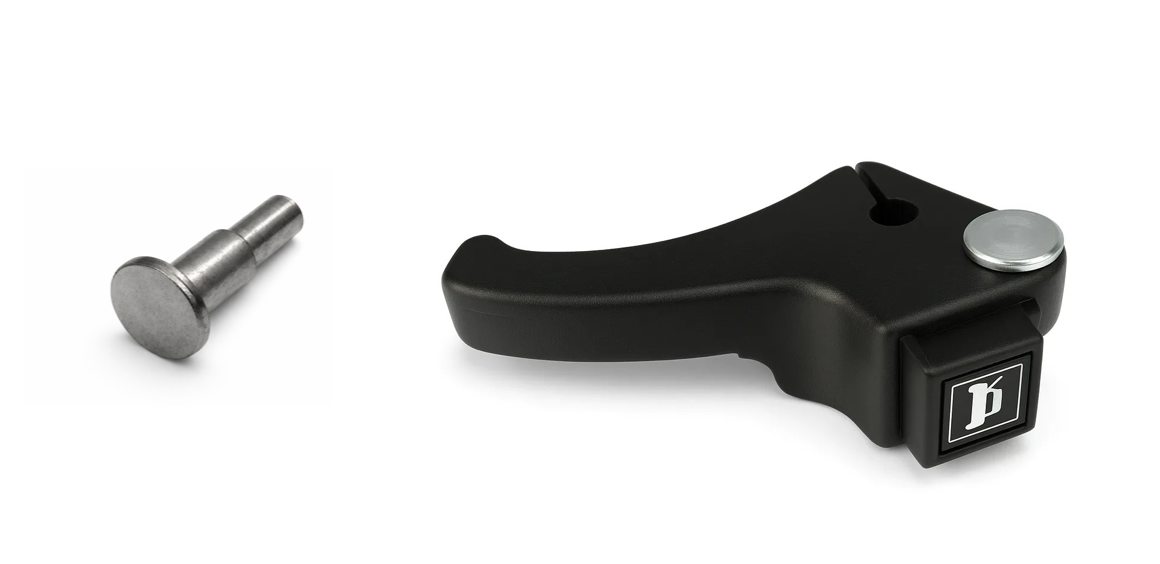
01 | The Lever Set
Mould the lever, then fit the pin.
The lever is moulded from 20% glass-filled Nylon-66 and moisture-conditioned before final assembly. The centre pin is fitted after moulding; it is not an insert in the moulding cycle. We also apply the product sticker shown on the lever.
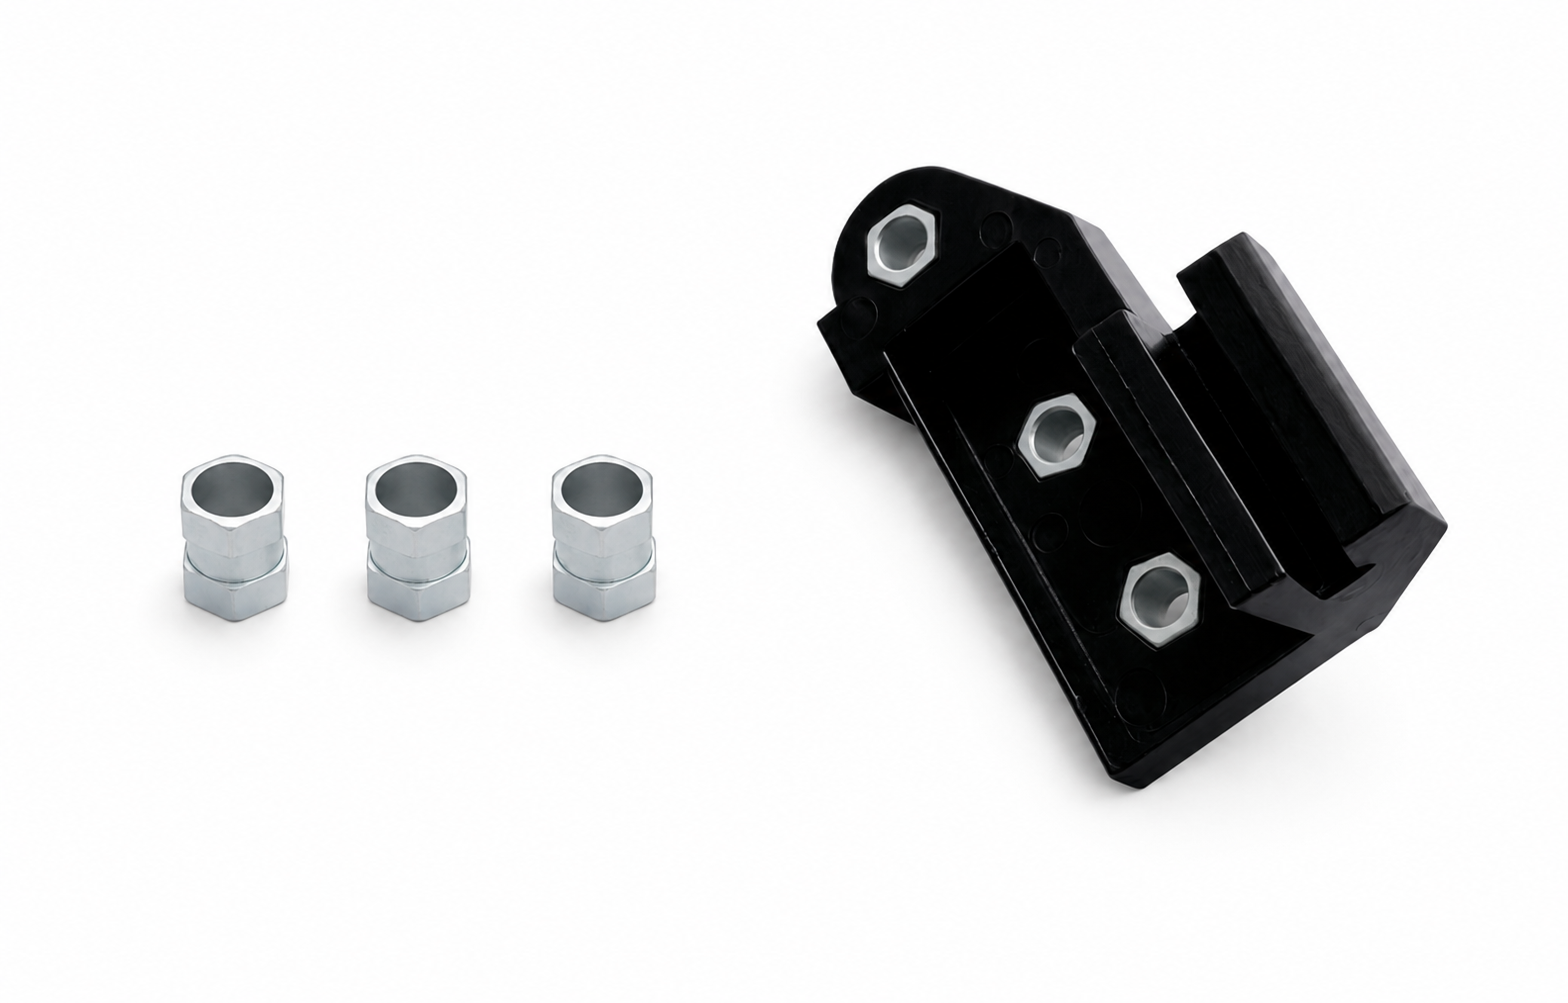
02 | The Bracket
Three plain-bore inserts in one moulding.
The bracket is moulded from unfilled Nylon-66 around three metal inserts in one cycle. These inserts have plain, unthreaded bores. The bracket is moisture-conditioned before it is assembled with the lever.
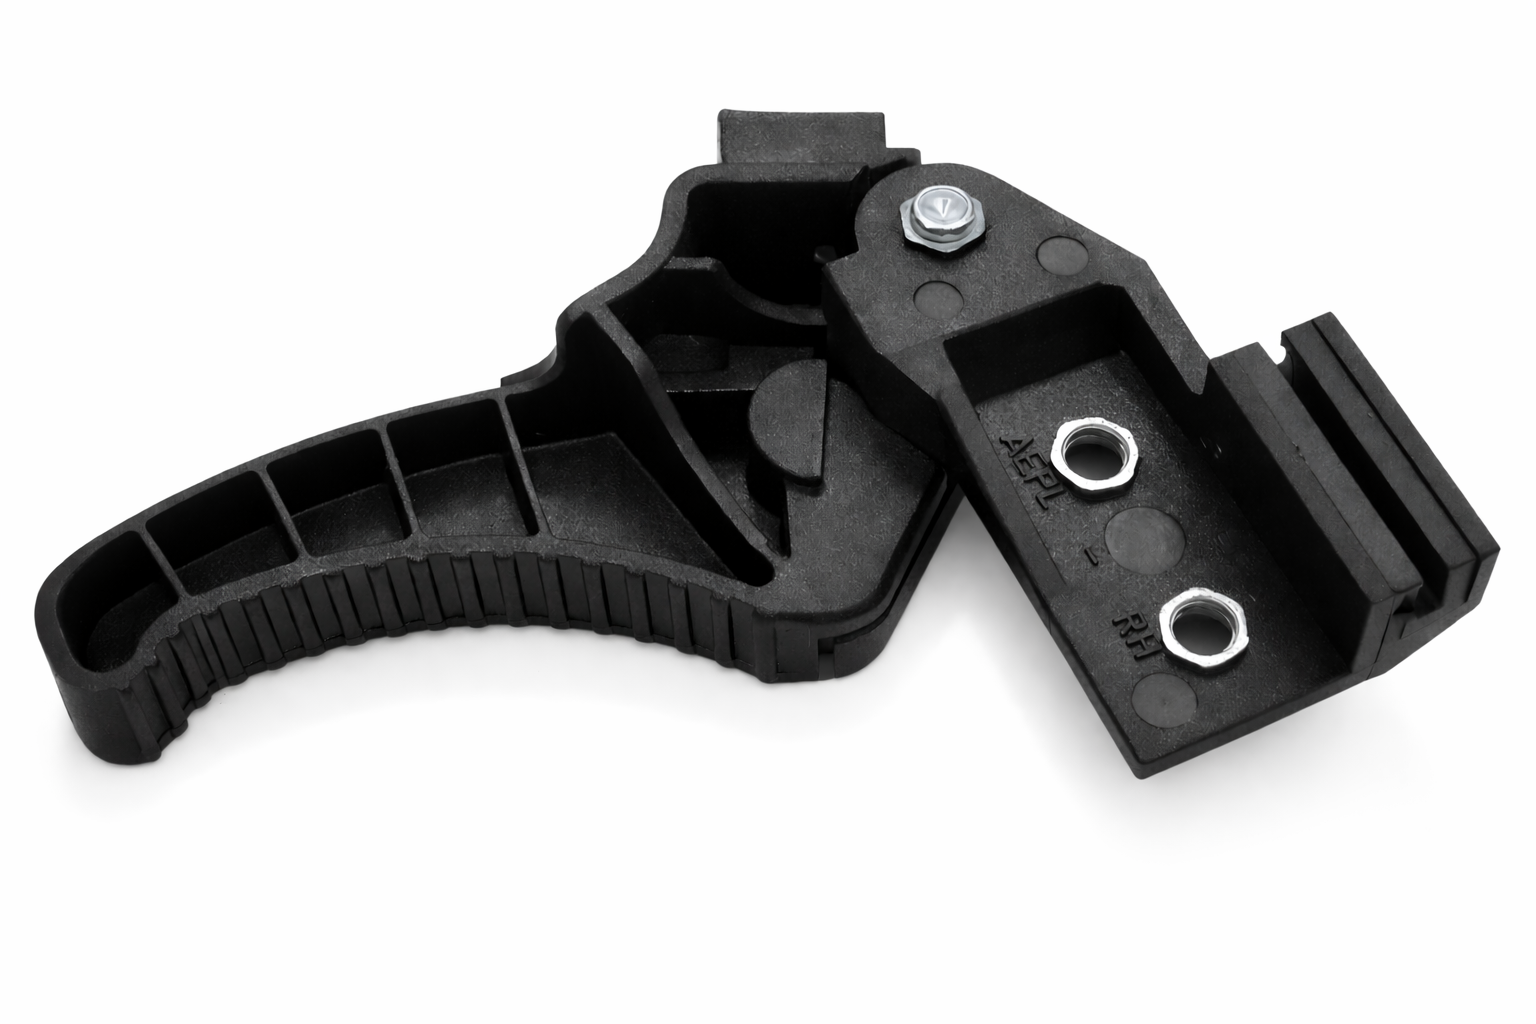
03 | The Finished Assembly
Conditioned parts, assembled in-house.
After conditioning, the lever and bracket are joined with the centre pin. Parshwa Plastics supplies the completed sub-assembly, with the moulding, conditioning and final fit handled in one production sequence.
The assembly requirement
Conditioning and insert position affect the final fit.
The moulded dimensions, insert positions and conditioning state all affect the final fit. Reviewing them together allows the assembly to be checked on the basis on which it will be supplied.
Scope of supply
One supplier for the completed assembly.
Parshwa Plastics handles component moulding, insert loading, moisture conditioning, sticker application and centre-pin assembly. The buyer receives the completed item from one supplier.